
Very happy with the purchase. I now have 16 of these. They work great.
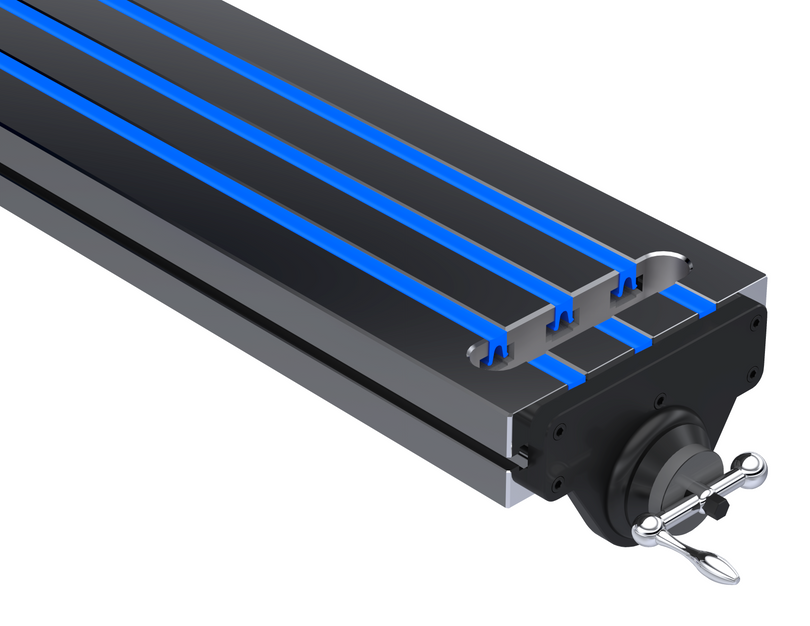
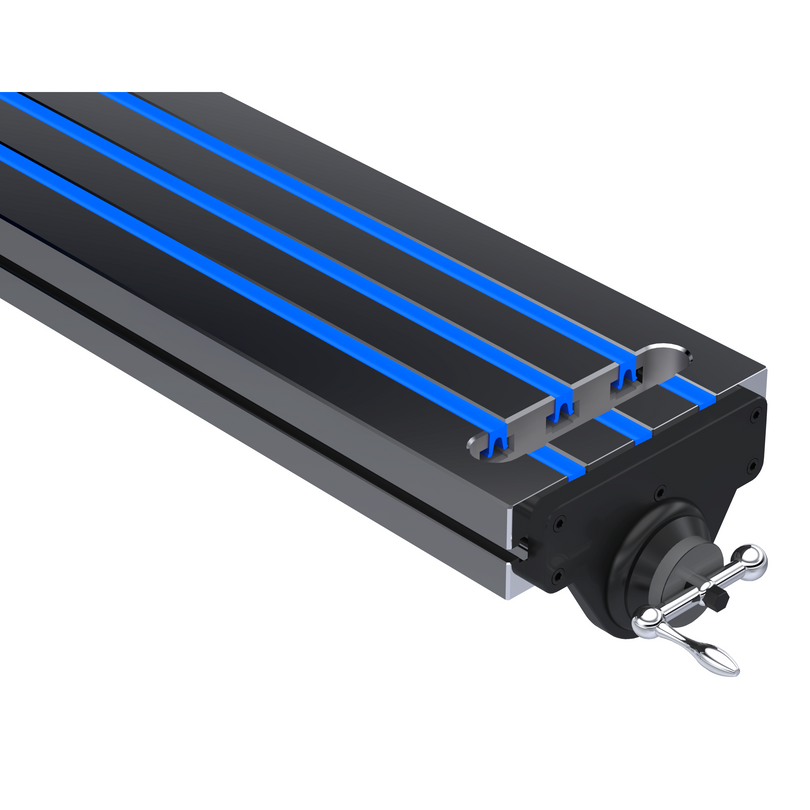
The Octane t slot chip guard is great, very heat and chip resistant, and a great addition to any mill. Highly recommend it.
Machinists use unique tools that each serve a purpose. Having the right tool for the job can make all the difference. Depending on the type of work you do, this could mean investing in entry level tooling, or high end. The saying "If you need a tool and don't buy it, you'll have paid for it and not have it." applies to machining more than any other profession.
The Caliper is a staple of the machining trade. The following links are our top picks for everyone from beginner to professional.
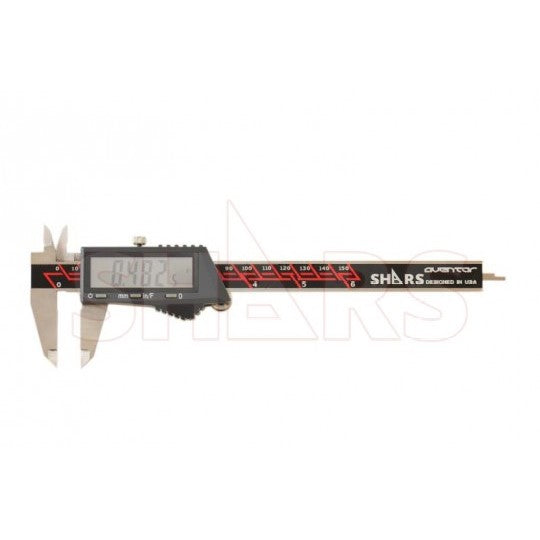
AVENTOR 6" LARGE SCREEN IP54 ELECTRONIC CALIPER - Affordable entry level caliper
AVENTOR 8" IP67 ELECTRONIC CALIPER - Affordable entry level caliper
MITUTOYO 8" IP67 ELECTRONIC CALIPER - Great Caliper we have used for years! Smooth action and consistent measurements.
MITUTOYO 12" IP67 ELECTRONIC CALIPER DATA OUTPUT - If you machine larger parts often like us, a quality 12" Caliper is essential. Data Ouput to PC!
When greater precision is required, the Micrometer is a great entry to inspecting higher end work. While Calipers can measure a wide size range both internally and externally, an entire set of Micrometers may be needed.
MITUTOYO 0-1" ENAMEL FRAME OUTSIDE MICROMETERS FRICTION THIMBLE 0.0001" - If you only need one good quality Micrometer, the 103 series is great.
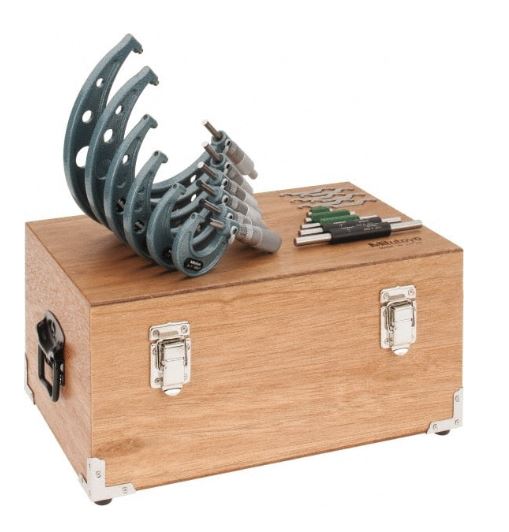
MITUTOYO 0-6" ENAMEL FRAME MECHANICAL OUTSIDE MICROMETER SET 0.0001 - This set is perfect for most shops and the one we reccomend most often. Everything needed is included.
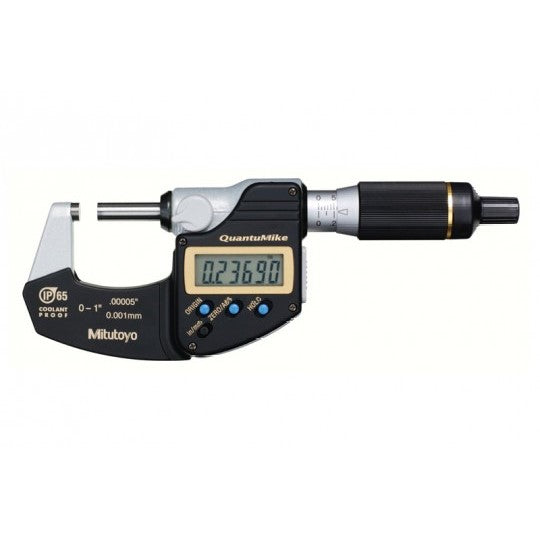
MITUTOYO 0-1" IP65 QUANTUMIKE ELECTRONIC OUTSIDE MICROMETER - The Quantumike is faster with 2mm / Rev. travel vs. the standard 0.5mm This Micrometer is excellent.
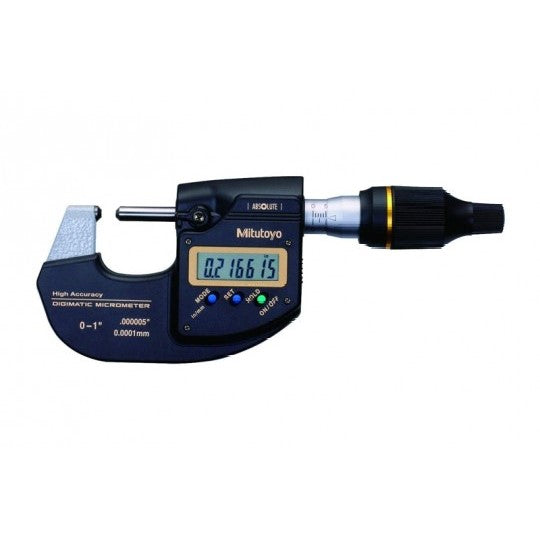
MITUTOYO 0-1" 0.0001MM MDH HIGH ACCURACY SUB-MICRON ELECTRONIC OUTSIDE MICROMETER - If you are working with extreme tolerances, this Micrometer has the accuracy.
This tool is great for quickly chamfering parts, the chamfer quality is close to that of a true machined finish.
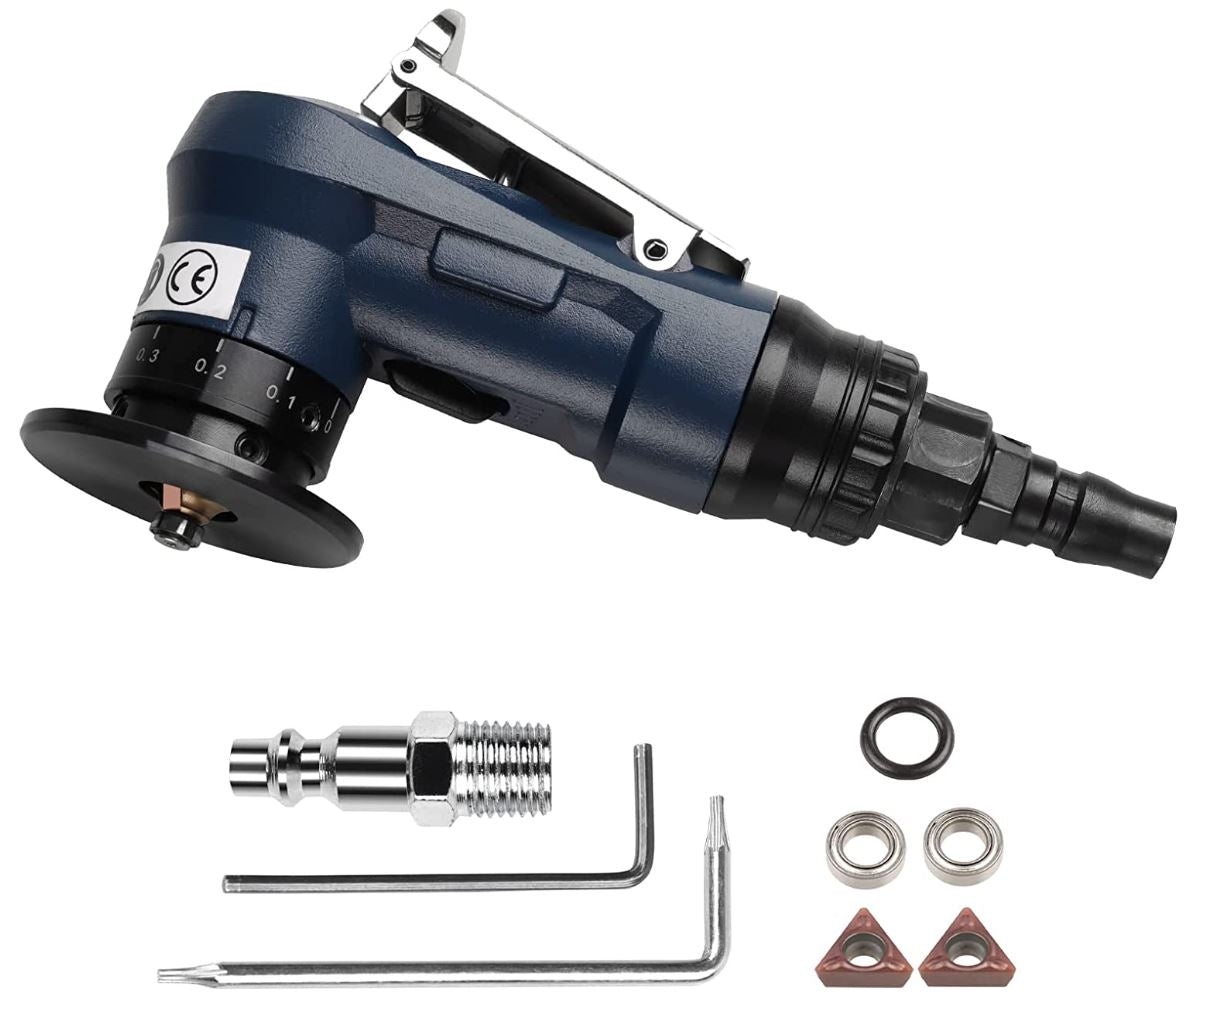
MINI PNEUMATIC CHAMFERING MACHINE,PORTABLE 45 DEGREE - This is a cheaper version of the SP Air deburring tool we use. By all accounts it works well too.
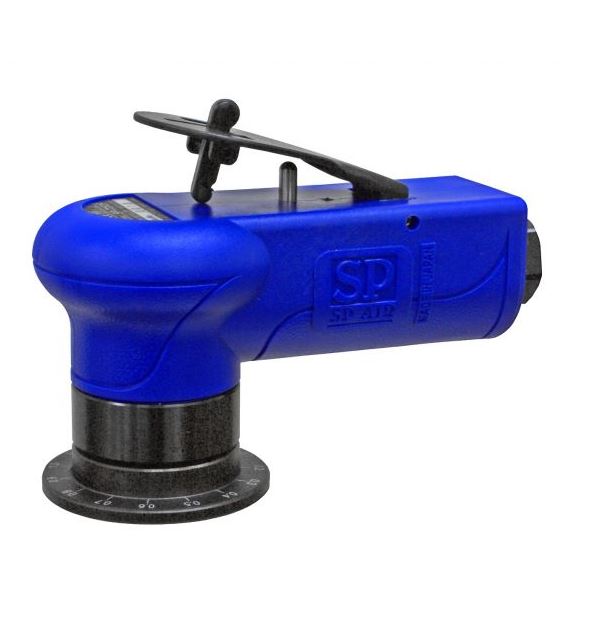
SP AIR TOOLS PALM BEVELING TOOL - This tool works great, it saves us a lot of time deburring parts off the waterjet especially. We recommend finding replacement inserts from Sandvik or similar once they wear out.
Measuring internally can be difficult in comparision to measuring outside dimensions. There are several tools of varying accuracy that are commonly used. Calipers are the most common, but not very accurate. Telescoping Gages can be more accurate in highly skilled hands, but Bore Gages are the most affordable entry into precision internal measuring.
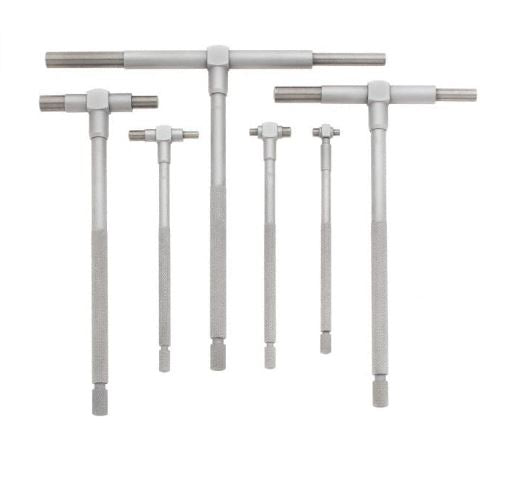
MITUTOYO 5/16"-6" TELESCOPING GAGE SET - Telescoping gages are affordable and fairly accurate with some training. We reccomend watching tutorials and reserving them for non-critical work.
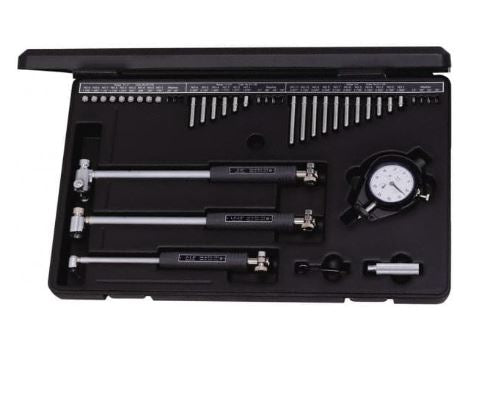
MITUTOYO 0.7 TO 6" DIAL BORE GAGE SET 0.0005" - Very good accuracy +- 0.00008" yet affordable. Bore gages are easy to use with some training. We have a tutorial video.
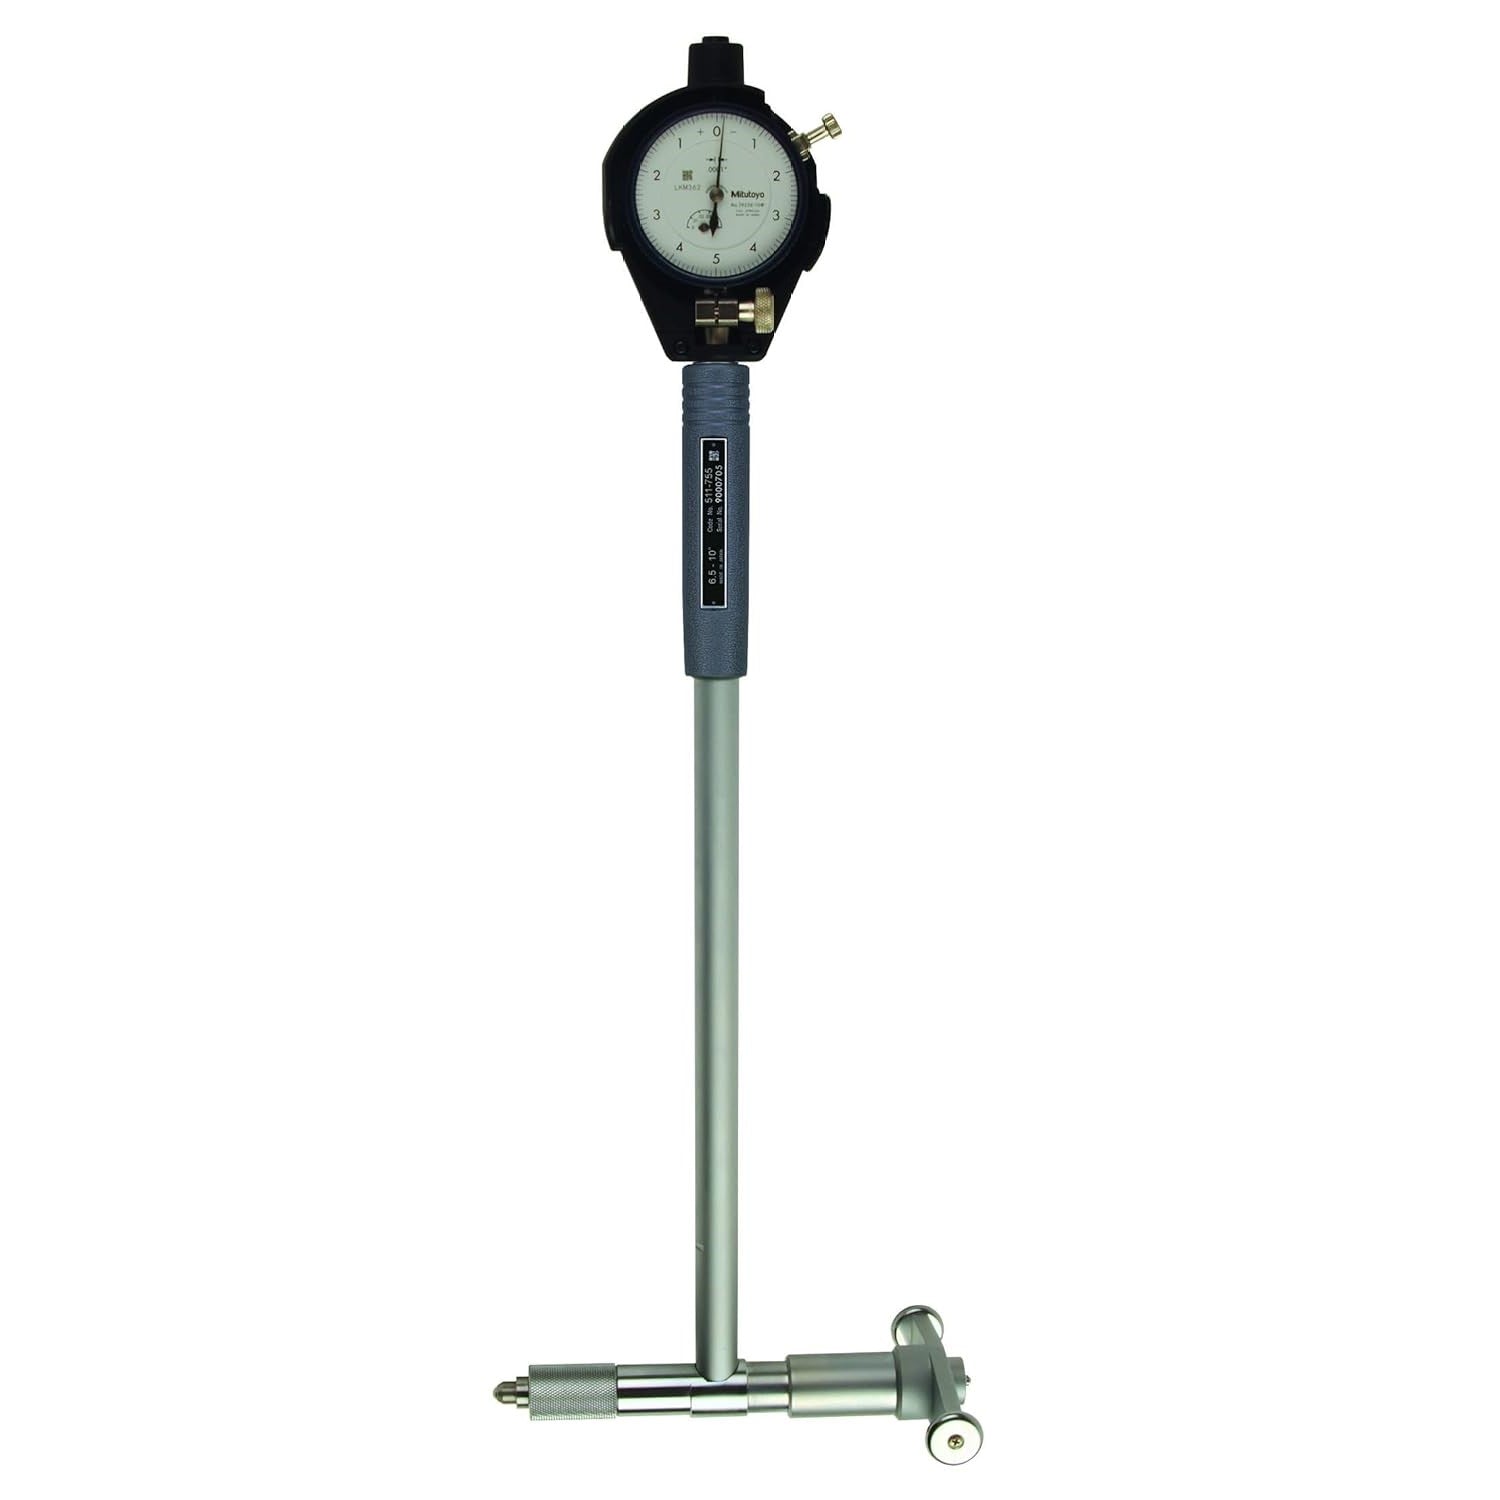
Mitutoyo 511-755-20 Bore Gage, 6.5"-10" Range, 0.00008" Accuracy, 0.0001" Graduation. Bore gages are easy to use with some training. We have a tutorial video.
Mitutoyo 511-756 Dial Bore Gage, 10 to 16 ", Stem Diameter 3/8 ", 0.0001" Graduation. Bore gages are easy to use with some training. We have a tutorial video.
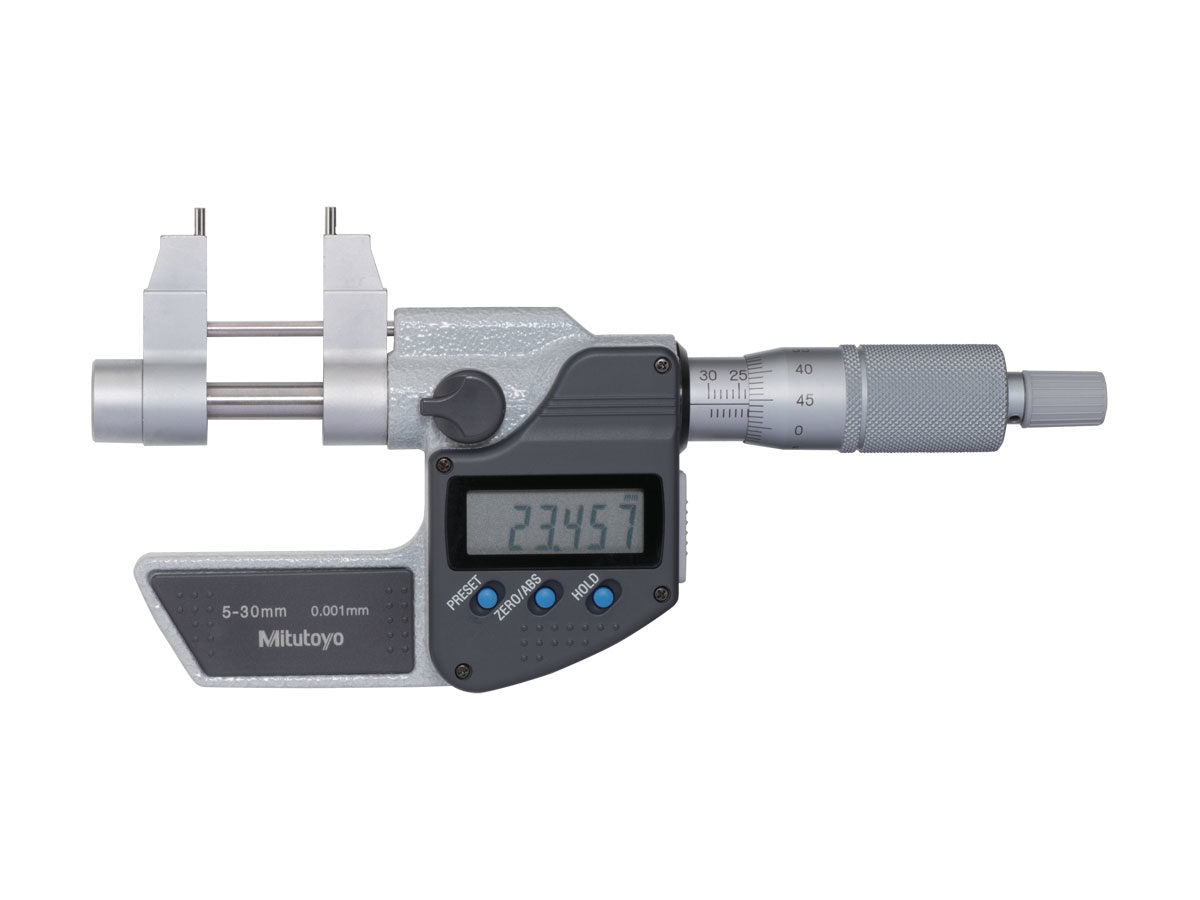
MITUTOYO 0.2 TO 1.2″ RANGE, 0.00005″ RESOLUTION, ELECTRONIC INSIDE & TUBULAR MICROMETER - Accurate for smaller work, generally up to 2.000" diamater. +-0.00025"
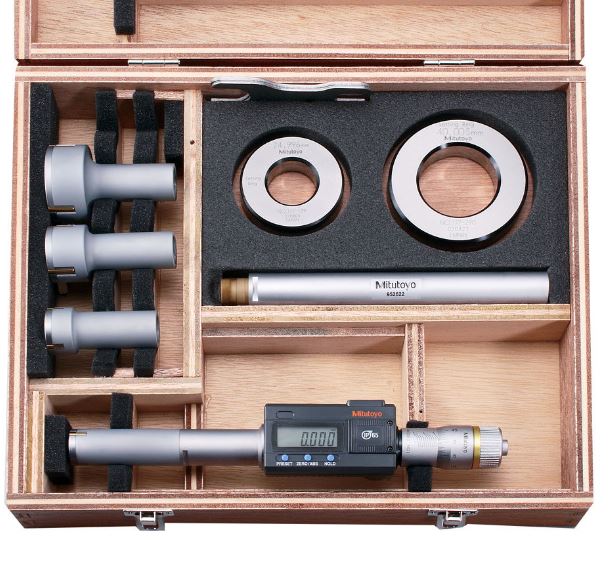
MITUTOYO THREE POINT INSIDE MICROMETER, 0.8-2" 0.00005" GRADUATION, +/-0.00015" ACCURACY (4 PIECE SET) - This style Micrometer is expensive, but easy to use and precise. Limited range means buying many sizes.
Having the right Indicator for the job is essential. Dial Indicators are ideally suited for large range indicating and easy to access angles. Dial Test Indicators are better suited for fine work in tight quarters such as squaring a vise, or inside a small bore. While it is possible to get by with one style or the other, it is much more difficult without both.
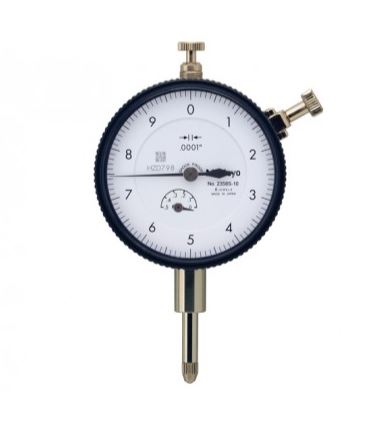
MITUTOYO 0.5" PRECISION AGD DIAL INDICATOR LUG BACK .0001" - Having a .0001" Dial Indicator with 0.5" of travel can come in very handy.
MITUTOYO 1" PRECISION AGD DIAL INDICATOR 3" DIAL LUG BACK .001" - A great all around Indicator you can rely on. The 3" dial makes this easy to read.
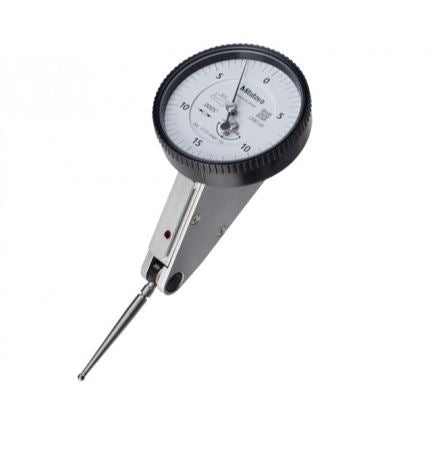
MITUTOYO .06" TRAVEL DIAL TEST INDICATOR .0005" - This Dial Test Indicator covers a wide range while still being very accurate and easy to use with the long stem.
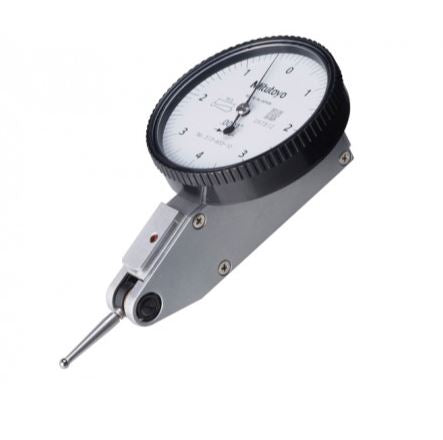
MITUTOYO .008" HORIZONTAL DIAL TEST INDICATOR .0001" - Having a tenths Indicator like this is essential for precision setups.
Holding an Indicator exactly where you need it has never been easier since the advent of the articulated arm. Gone are the days of dealing with rigid posts and multiple knobs to tighten down. Most of these arms feature a fine adjust at either the top or bottom. Fine adjust at the bottom (FAB) arms are easier to fine tune, especially when using a .0001" Indicator.
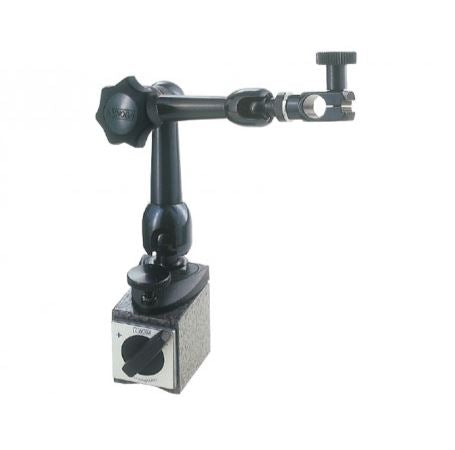
NOGA NF10433 70 LB MAGNETIC INDICATOR HOLDER MINI W/ FINE ADJUSTMENT AT BASE (FAB) - Fine adjustment at base allows for more precise control over the Indicator positioning.
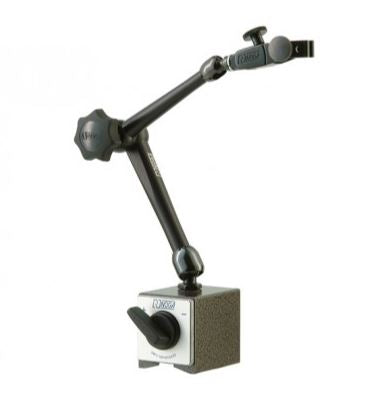
NOGA DG61003 176 LB MAGNETIC FORCE INDICATOR HOLDER - We have been using this long reach base for years. Adjustments are a bit more difficult than models with a fine adjust at the base.
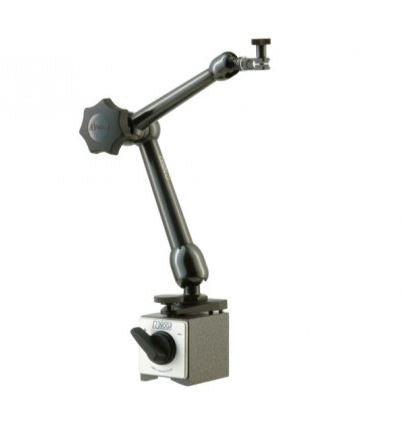
NOGA MG10533 176 LB MAGNETIC FORCE INDICATOR HOLDER MAGNETIC BASE W/ FINE ADJUSTMENT AT BASE (FAB) - This is probably the best all around base on the market if you could only choose one.
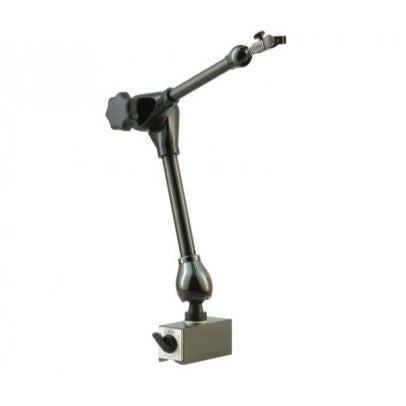
NOGA MA61003 292 LBS MAGNETIC FORCE BIG BOY INDICATOR HOLDER - This base is big and heavy, we actually use it for automated welding among other things!
Measuring the height of a part can actually be one of the more difficult measurements overall. Having a good flat surface such as a surface plate and a height gauge are the next best thing to a CMM.
Even the most accurate measuring tools rely on calibration tools to verify the settings before use. These setup tools are calibrated in a lab setting and guaranteed for their accuracy.
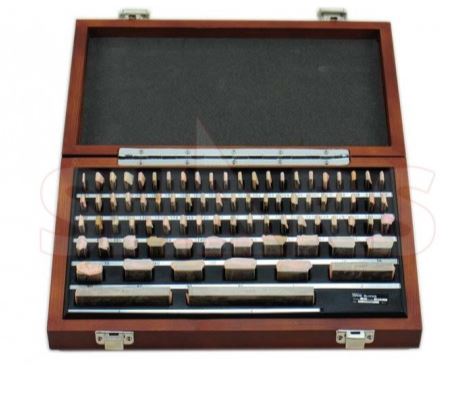
GRADE AS-1 .050 TO 4.000" 81 PCS RECTANGULAR GAGE BLOCK SET - This set is affordable and accurate enough for most shops working with +-.0005" tolerances.
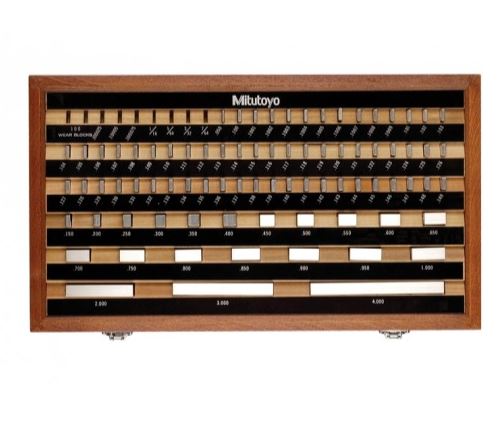
MITUTOYO 81 PCS 0.05 TO 4.000" GRADE AS-0 RECTANGULAR GAGE BLOCK SET - At $2,000 more than the first set of blocks, every decimal place is costly. If you need extreme precision there is no exception.
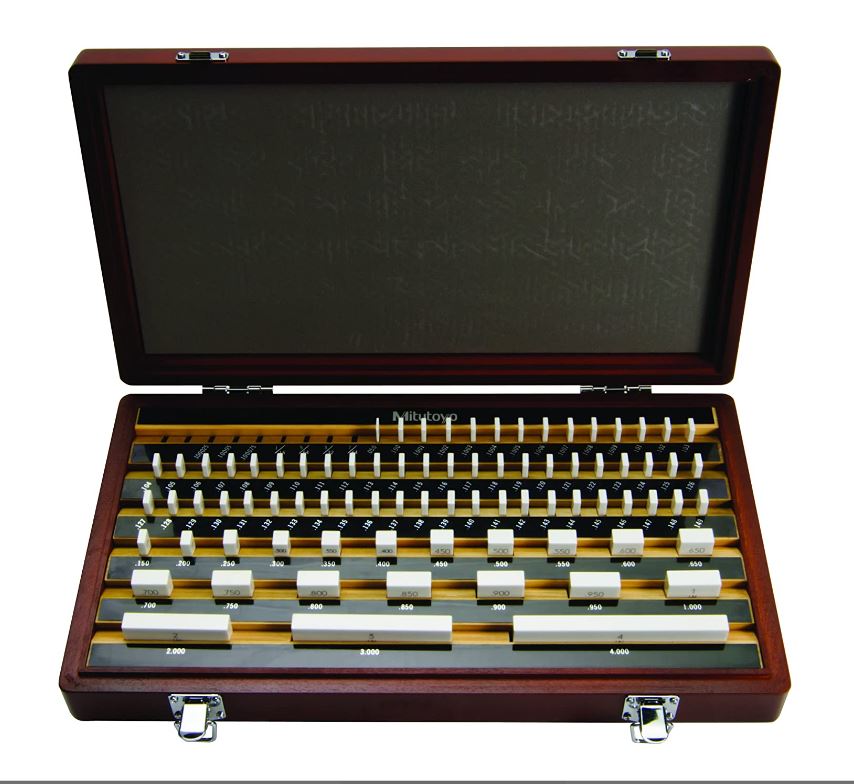
MITUTOYO CERAMIC 81 PCS 0.05 TO 4.000" GRADE AS-00 RECTANGULAR GAGE BLOCK SET - At $4,700 more than the previous set of blocks, these ceramic gages are on another level for accuracy.
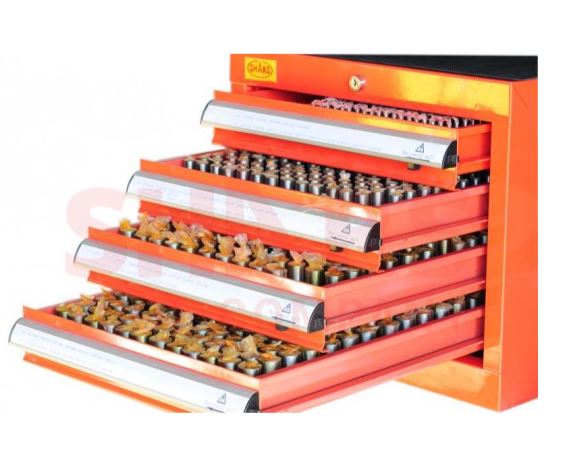
0.011-1" 990 PC CLASS ZZ PIN GAGE SET STEEL CABINET WITH FOUR DRAWERS FOR MINUS - This affordable set of Pin Gages can make life a lot easier inspecting parts. Consider adding a go / no-go pin gage handle to hold two sizes.
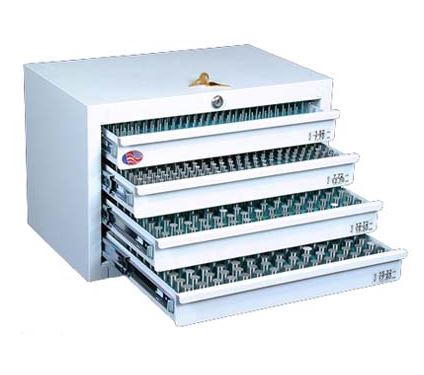
0.011-1" 990 PC CLASS Z PIN GAGE SET STEEL CABINET WITH FOUR DRAWERS FOR MINUS
Having the right setup for your vises can prevent a lot of frustration. These are our top picks for general shop work.
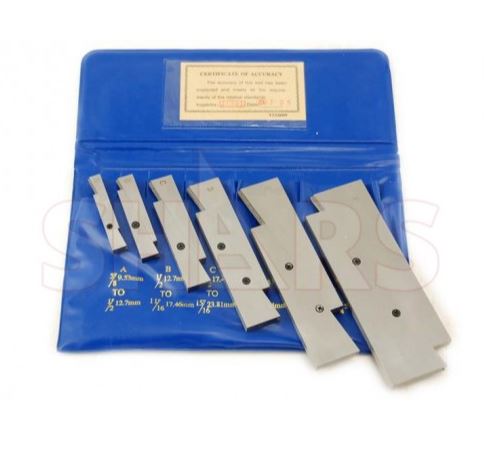
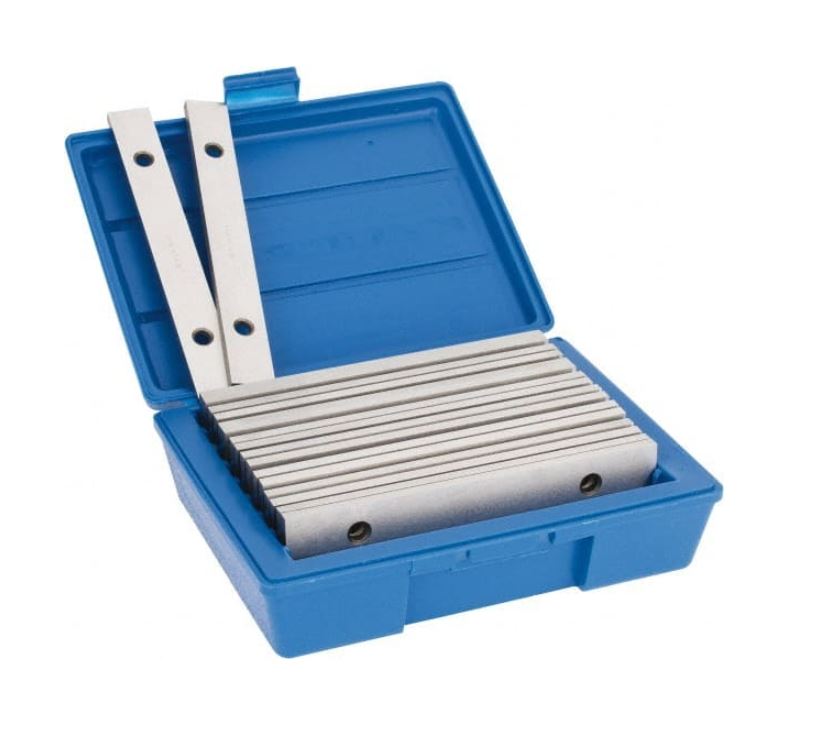
SHARS ADJUSTABLE PARALLEL SET - We use this set for workholding setups and fabircation, it is great always having the perfect spacer.
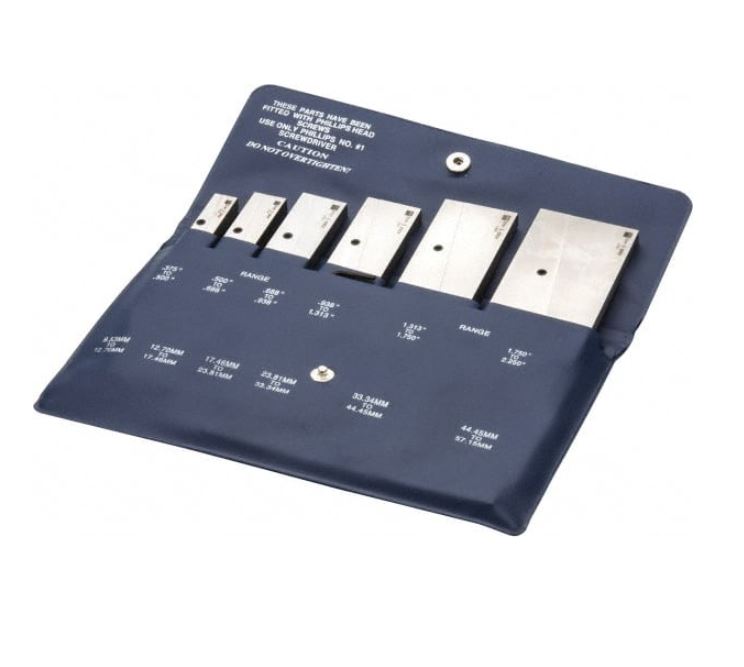
TESA BROWN & SHARPE
3/8 TO 2-1/4 INCH ADJUSTABLE PARALLEL SET - This is our go-to set for everyday use. They are accurate enough for measuring and slide smoothly.
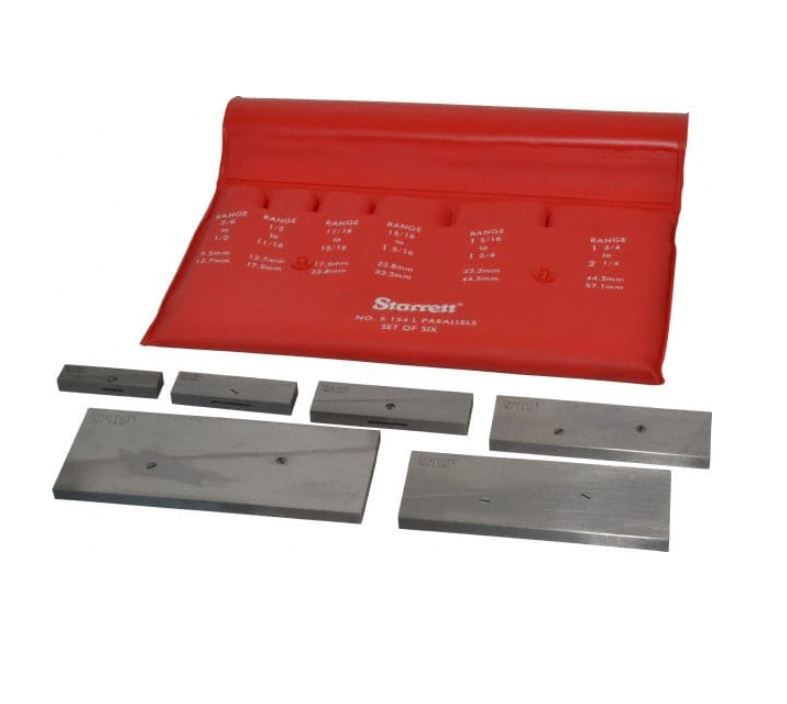
STARRETT
3/8 TO 2-1/4 INCH ADJUSTABLE PARALLEL SET
1-3/4 TO 5-1/16 INCH LONG, 9/32 INCH THICK,
INCLUDES CASE, 6 PIECES
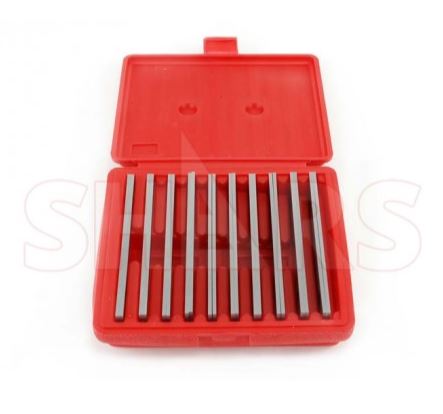
1/8 INCH THICK STEEL PARALLELS - This affordable set of thin parallels is great for general work.
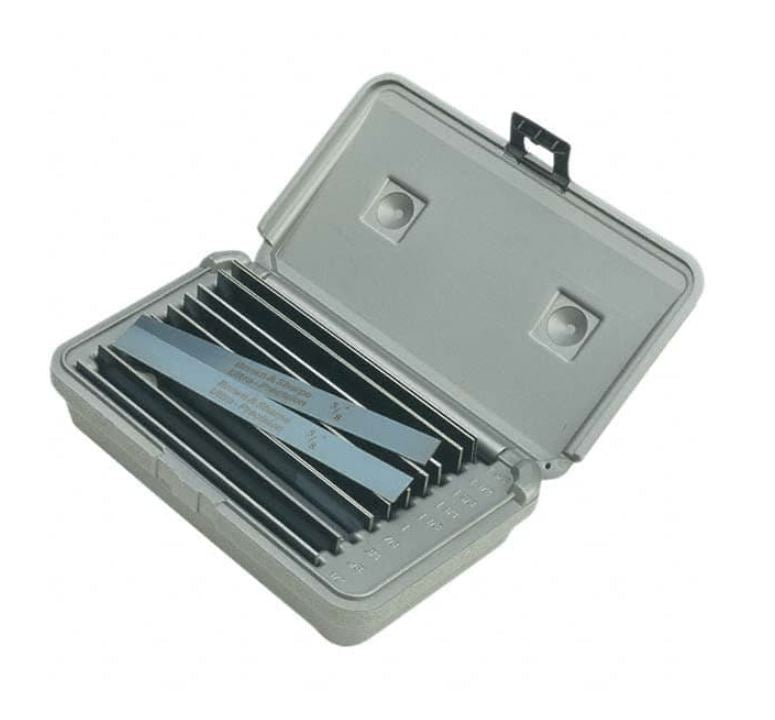
TESA BROWN & SHARPE
20 PIECE, 6 INCH LONG X 1/8 INCH THICK,
THIN PARALLEL SET - With a Parallelism of 0.0002", this set has the accuracy for precision work.
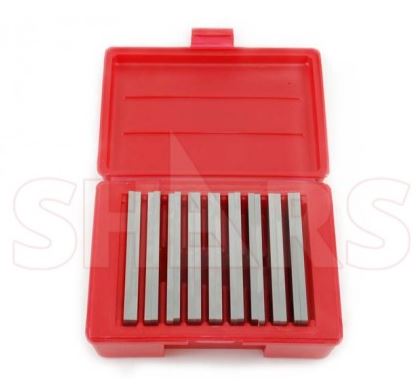
Shars 1/4" STEEL PARALLELS WITH PLASTIC CASE - This set is hard to beat for general work, we have multiple sets for use all around the shop.
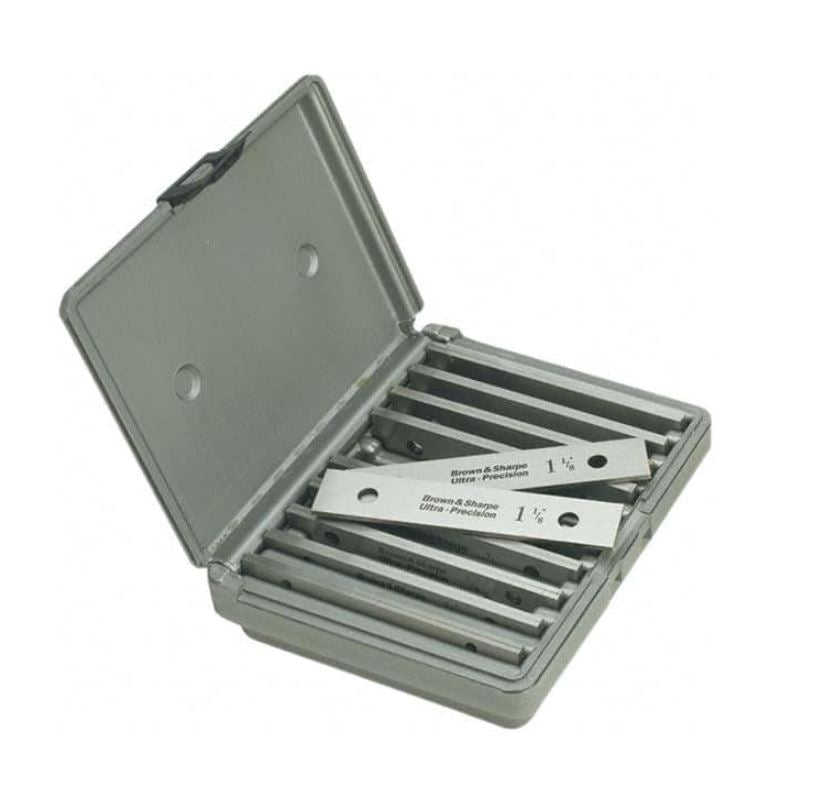
TESA BROWN & SHARPE
20 PIECE, 6 INCH LONG X 1/4 INCH THICK,
THIN PARALLEL SET - With a Parallelism of 0.0002", this set has the accuracy for precision work.
KURT PARALLEL SET, 8" • 1.000″, 1.250″, 1.375″, 1.500″,
1.625″, 1.750″, 1.875″, 2.000″,
2.125″ Heights
• 0.250″ ±0.002″ Thickness.
• 0.0002″ Parallelism.
Speed handles make opening and closing your vises significantly faster. Having the right workstop for your application makes repeatable setups easier.
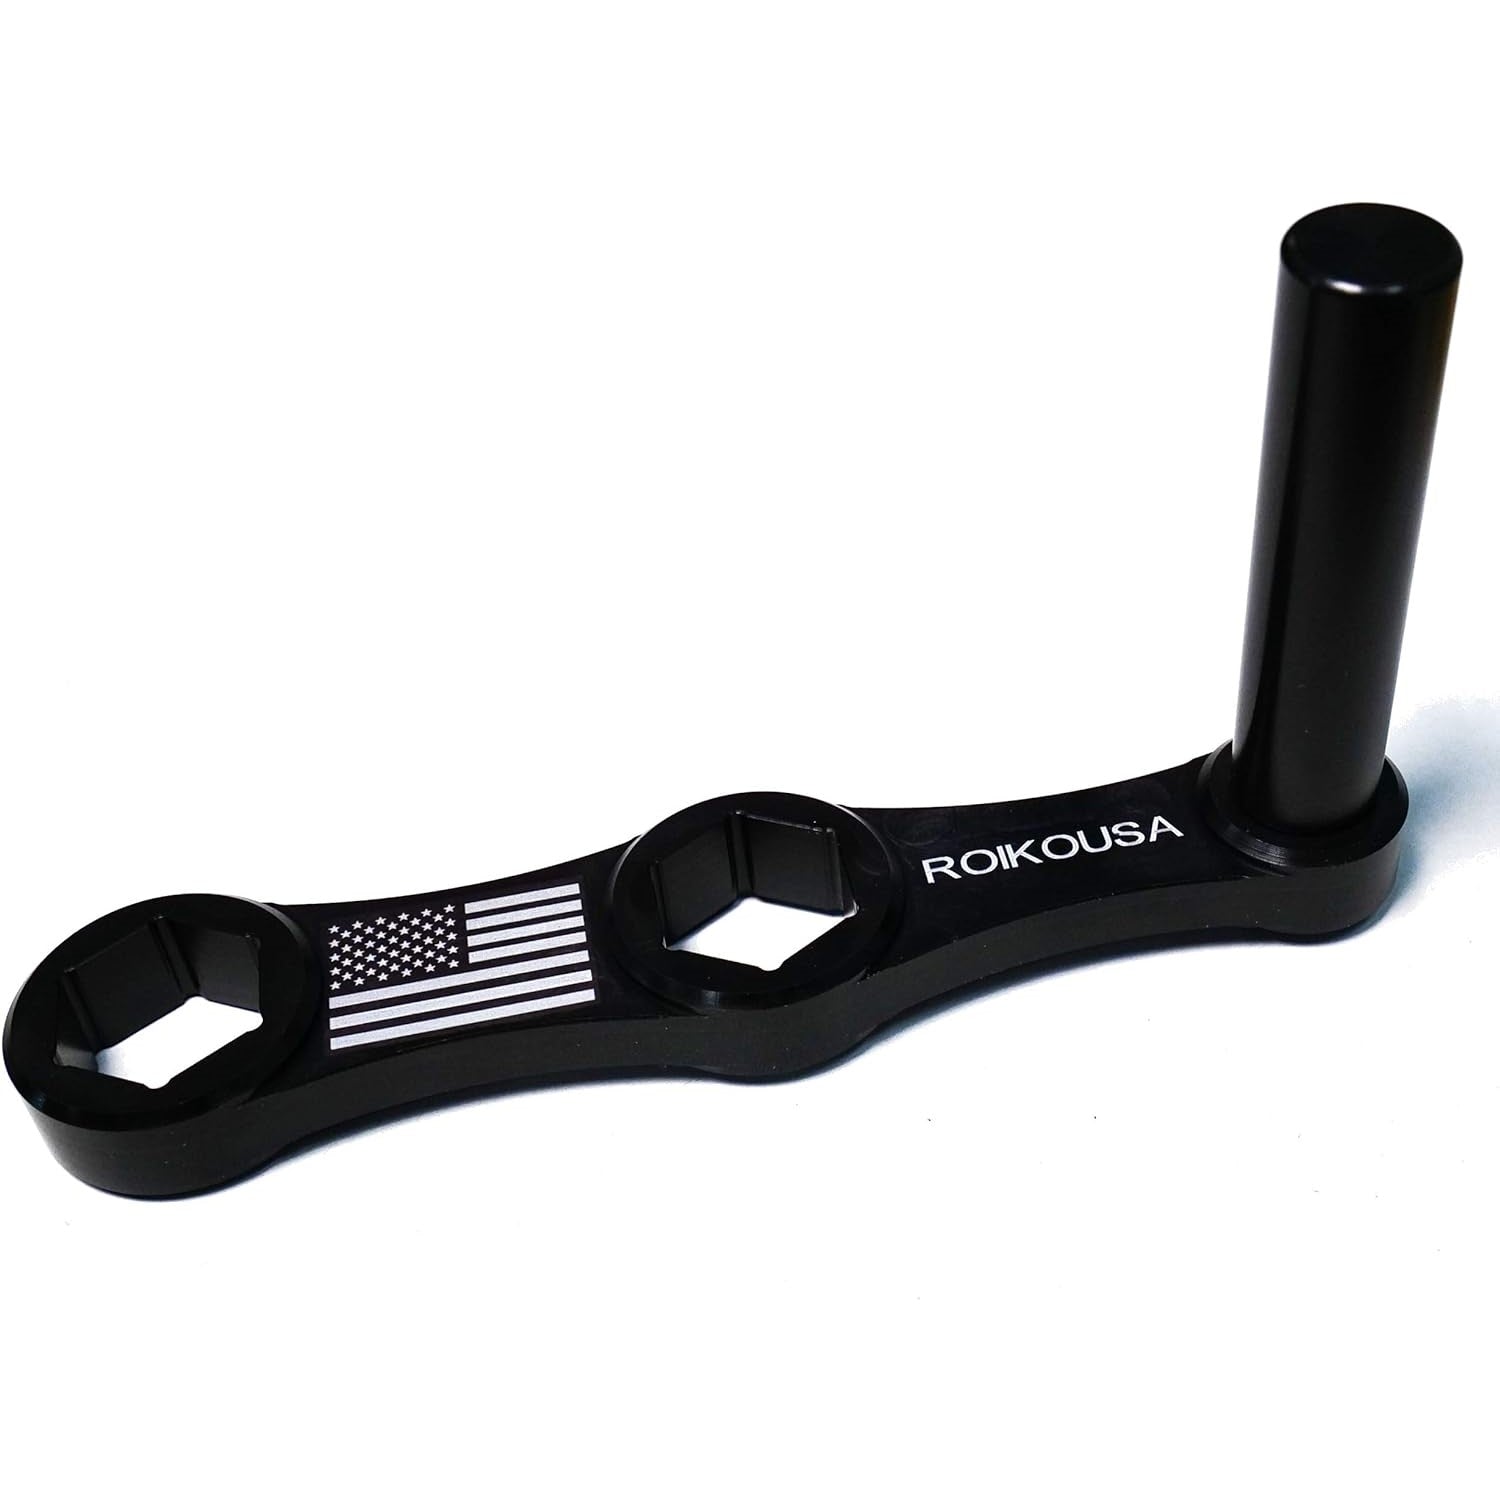
Speed Handle With BEARING Handle Spins
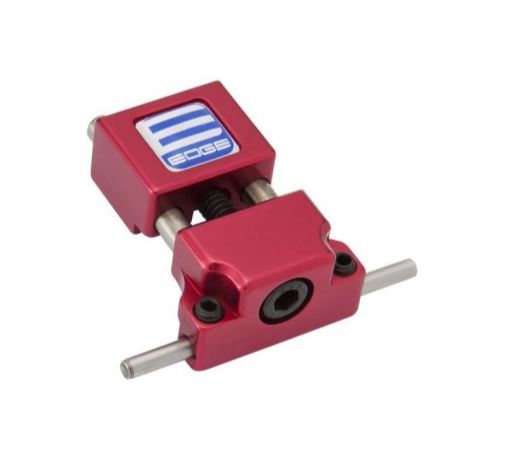
EDGE TECHNOLOGY VISE JAW STOP - This stop attaches direct to the vise jaw. The rod is positioned below the jaws top surface for clearance.
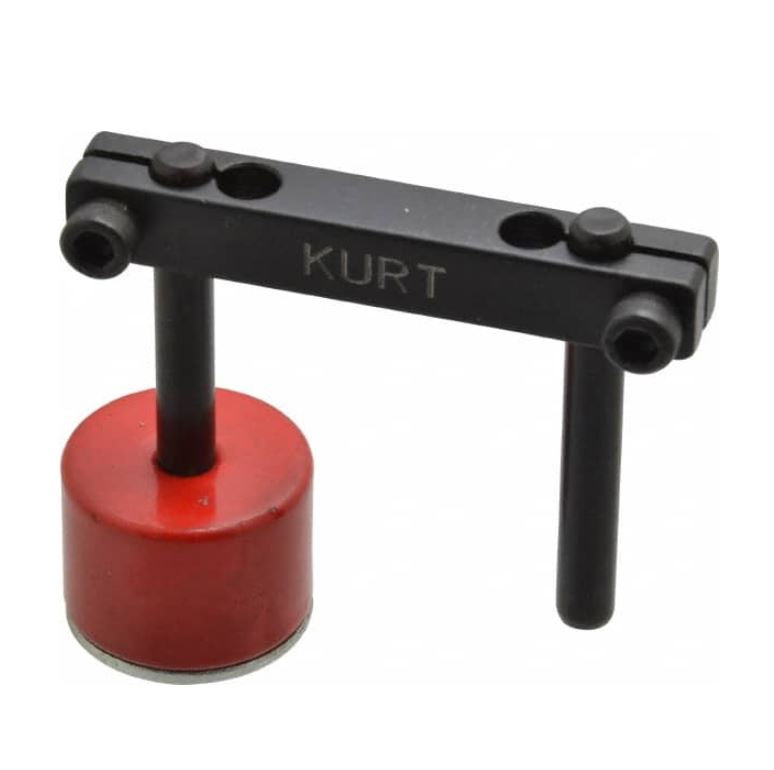
KURT MAGNETIC VISE WORK STOP - This is our most used workstop, it is easy to place and remove in seconds making it versatile. Remember to remove the metal cover from the magnet.
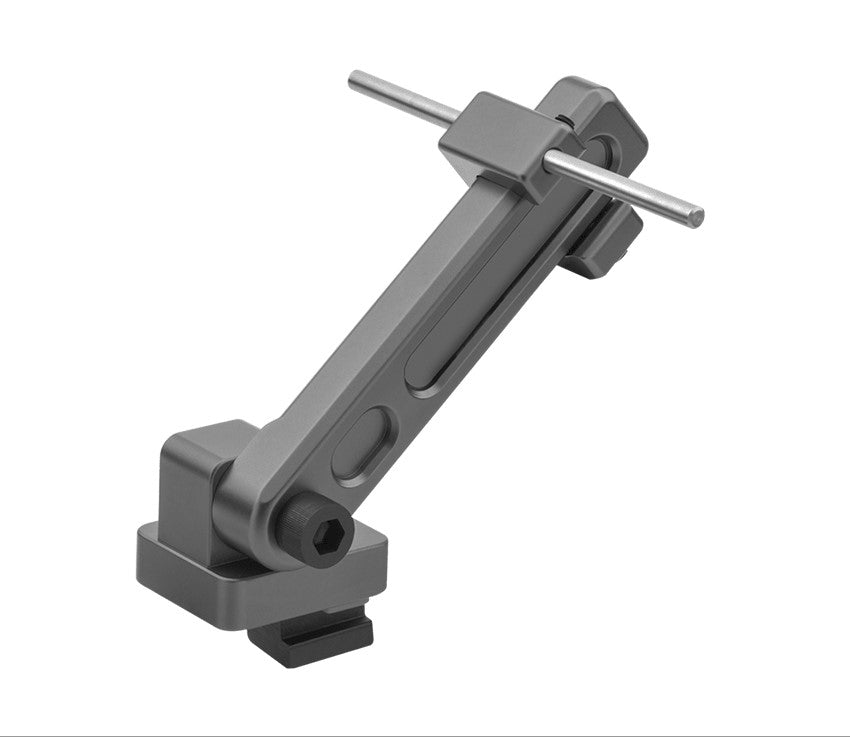
WORKSTOP TILTS 180° AND HAS AN ADJUSTABLE STOP PIN THAT SLIDES IN AND OUT FOR PRECISE POSITIONING.
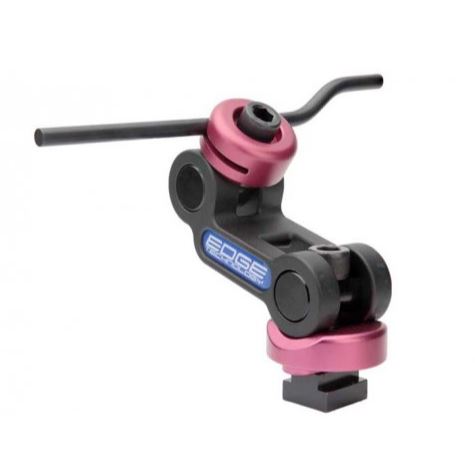
EDGE TECHNOLOGY MULTI AXIS STOP
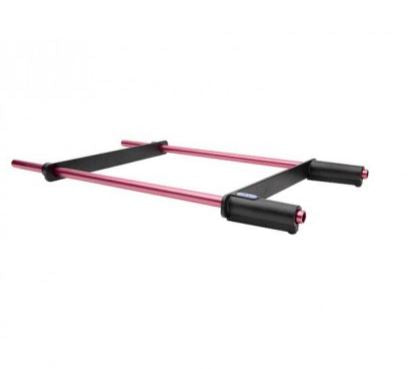
EDGE TECHNOLOGY PARALLEL SEPARATOR
Doing any type of manual machining almost certainly requires a variety of punches. Our shop does a lot of fabrication as well which means they get used daily.
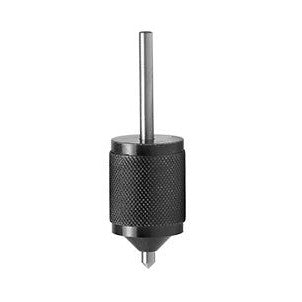
CENTER-LOCATING PUNCH FOR UNTHREADED HOLES
FOR 3/16" TO 1-1/16" AND 5MM TO 27MM DIAMETERS - We have been using punches like this for decades, they can replace a whole drawer of punches.
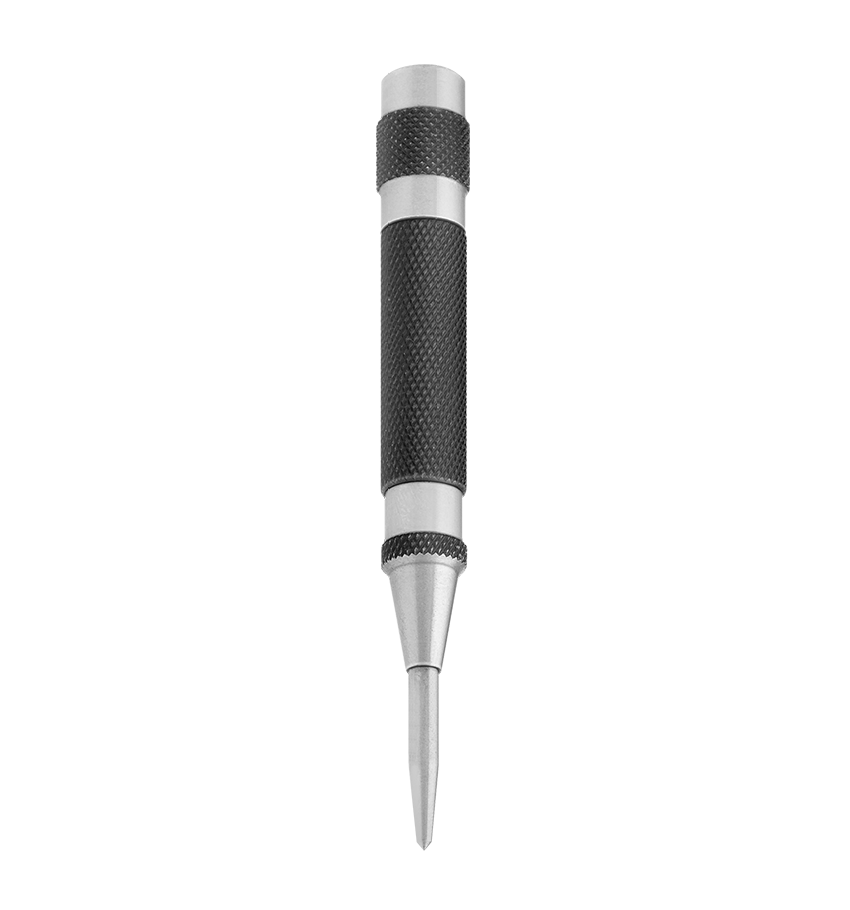
SPRING-IMPACT MARKING PUNCH
STARRETT 18C WITH STEEL HANDLE - These punches are ideal for light marking. If you need a heavier mark it is best to follow up with a standard punch.
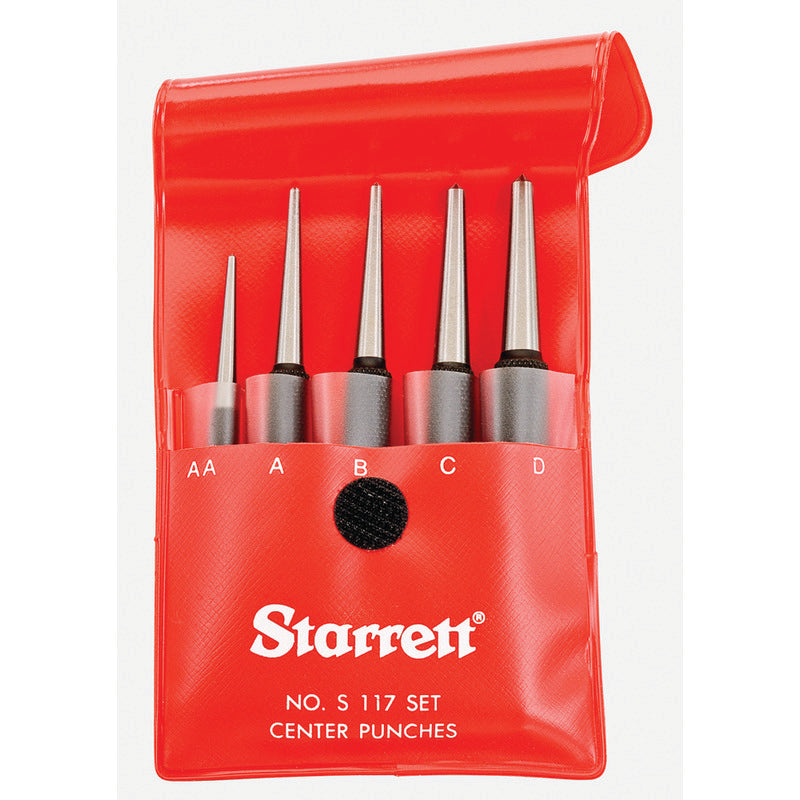
5 PieceStarrett Marking Punch Set - Having a good set of punches like these can come in handy, they are a staple of any shop.
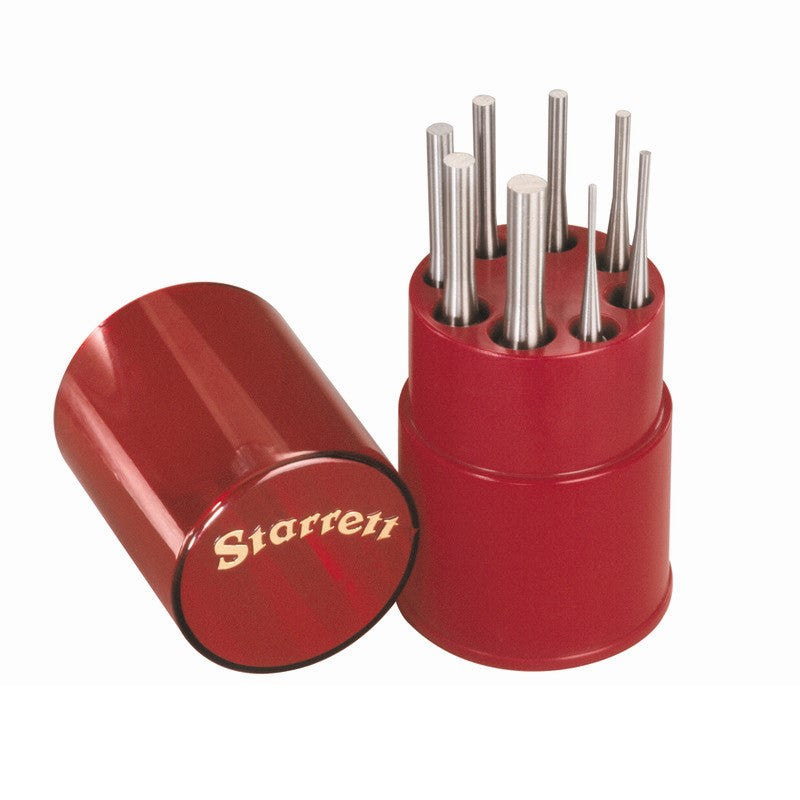
STARRETT 8 PIECE PIN-REMOVAL PUNCH SET - We use these punches daily, having quality steel punches that don't deform easily is important.
While many tools can be used to measure depth, having a dedicated tool can come in handy. Some parts have features which make obtaining an accurate measurement difficult or impossible otherwise.
Machinists rely on their measuring tools to determine whether a machined feature is within tolerance or not, the latter can be costly.
Tools ranging from a simple Caliper, to highly accurate coordinate measuring machines. Many common measuring tools are subjective, relying on human input being repeatable to be reliable. One of the most affordable solutions to this dilemma is a ratcheting mechanism which creates a more repeatable input from user to user, common to many Micrometers.
For this reason, Micrometers are a great entry to precision work. Many Micrometers have a resolution of .0001" or one tenth of a thousandths, but an accuracy of +- .0001" making measurements near the edges of a tolerance risky. Some models go one step further with a resolution of .00005" / .001mm and an actual listed accuracy of .00005" making them much better suited for precision work where every micron (μm) counts.
The rule of thumb is to divide your tolerance range by 10 when selecting the resolution needed from a measuring device. A gauge or measuring device should ideally be 10xs as accurate as the tolerance. This is a widely accepted industry standard.
{Example (+-.0005") .001" total tolerance should be measured with a resolution of .001 ÷ 10 equaling .0001"} Micrometers have a. 0001" resolution and are often used for such measurements as confident readings can be taken without much training. A caliper often has a resolution of .001" meaning a tolerance less than +-.005" may be risky to measure, .001*10=.010"
A tolerance of +-.0001" (one tenth of a thousandths) would require .00001" resolution which common micrometers cannot provide.
At this close of tolerance temperature begins to play a major role. A measurement taken on a climate controlled coordinate measuring machine at 68° F may be vastly different in the field. Parts with tolerances closer than +-.0002" should be designed around the actual operating temperature of the intended use.
For the average shop, guaranteeing tolerances closer than +- .0005" would require investing in the right measuring systems. Aiming for the middle of a tolerance is usually reccomended. Imagine a scenario where micrometers are being used to measure a .001" total tolerance. Is the part scrap if it is measured at the upper or lower end of the tolerance? Impossible to say without a finer resolution measuring device. Surface finish also plays a major role in sizing, a surface should be uniform throughout to guarantee a dimension.